Legacy PLC-5 SCADA Integration Solution — Allen-Bradley 1775-GA | DH+ Communication Module
In legacy-heavy discrete manufacturing and process plants, communication failures between PLC-5 racks and supervisory systems are among the costliest unplanned events on the floor. Industrial reliability surveys consistently show that network-layer faults account for 18–25% of unplanned downtime in facilities running mixed-generation control architectures. When a PLC-5 rack loses its link to the Data Highway Plus (DH+) backbone, operators lose SCADA visibility, historians stop logging, and production halts — often for hours while technicians trace the fault to a failed communication module.
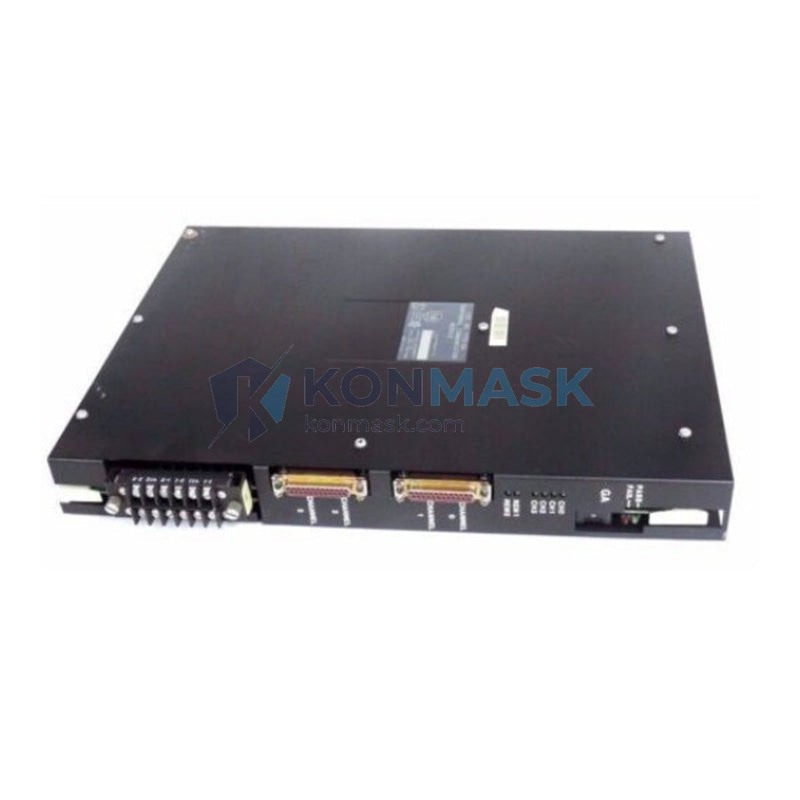
The Allen-Bradley 1775-GA Communication Module restores and sustains that critical link. Designed specifically for the PLC-5 family, it provides a dedicated DH+ network interface that integrates seamlessly into Rockwell Automation control architectures — enabling reliable peer-to-peer messaging, SCADA polling, and MES data exchange across multi-drop networks at up to 57.6 Kbps. For facilities that cannot afford a full migration to ControlLogix, the 1775-GA is the proven, cost-effective path to keeping legacy infrastructure communicating at specification.
Where This Product Is Used
Automotive Assembly & Body Welding
Robotic welding cells and transfer lines coordinated by PLC-5 racks rely on DH+ for inter-PLC messaging and fault reporting. The 1775-GA maintains the network node in environments with ambient temperatures up to 60 °C and high EMI from welding inverters. Typical workloads: weld-sequence interlocking, robot cell fault annunciation, cycle-time data to MES. Applicable standard: ANSI/RIA R15.06 robot safety integration.
Oil & Gas Upstream / Midstream
Remote wellhead RTUs and compressor station PLCs use DH+ to report to SCADA hosts over long cable runs (up to 3,048 m at 57.6 Kbps). The 1775-GA supports the multi-drop topology required for trunk-and-drop field wiring across large plant footprints. Typical workloads: pressure/flow polling, ESD status reporting, compressor run-hour logging. Applicable standard: API RP 554 process control systems.
Pulp & Paper / Continuous Process
Paper machine drive sections and stock preparation systems use PLC-5 racks for coordinated speed control. The 1775-GA enables the historian server to poll all nodes for process data trending and SPC analysis without interrupting the control scan cycle. Typical workloads: basis-weight trending, broke-detection alarming, drive-speed synchronization data. Applicable standard: TAPPI TIP 0404-56 control system reliability.
Water & Wastewater Treatment
Lift stations, clarifier drives, and chemical dosing systems managed by PLC-5 controllers communicate status to SCADA via DH+. The 1775-GA provides the node interface in corrosive, high-humidity enclosures (up to 95% RH non-condensing). Typical workloads: chlorine dosing feedback, pump run/fault status, flow totalization to SCADA. Applicable standard: AWWA M2 instrumentation and control.
Food & Beverage Processing
Filling lines, pasteurizers, and CIP systems use PLC-5 for recipe management and batch sequencing. The 1775-GA links the PLC rack to MES systems for OEE data collection, downtime tracking, and batch record generation. Typical workloads: CIP cycle logging, filler speed data, batch ID handshake to ERP. Applicable standard: FDA 21 CFR Part 11 electronic records (via MES layer).
Power Generation & Utilities
Boiler management systems, turbine auxiliaries, and switchgear control panels in power plants use PLC-5 racks with DH+ for distributed I/O coordination and alarm annunciation. The 1775-GA sustains the network node through wide voltage transients and high-vibration environments. Typical workloads: boiler drum-level alarming, turbine auxiliary sequencing, switchgear status to DCS. Applicable standard: NERC CIP-005 electronic security perimeter (network segmentation).
Technical Specifications
| Part Number | 1775-GA |
| Manufacturer | Allen-Bradley / Rockwell Automation |
| Series | PLC-5 |
| Module Type | Data Highway Plus (DH+) Communication Module |
| Network Protocol | Data Highway Plus (DH+) — Rockwell token-passing protocol |
| Baud Rates | 57.6 Kbps / 115.2 Kbps — higher baud rate reduces polling latency in dense SCADA networks |
| Max Network Nodes | 64 nodes per DH+ link — supports large multi-drop topologies in plant-wide SCADA networks |
| Max Cable Length | 3,048 m (10,000 ft) at 57.6 Kbps — covers large plant footprints in oil & gas and utilities without repeaters |
| Connector Type | DH+ terminal block (Belden 9463 or equivalent shielded cable) |
| Backplane Interface | PLC-5 I/O chassis backplane (1771 series) |
| Operating Temperature | 0 °C to +60 °C — suitable for non-air-conditioned industrial enclosures in automotive and process plants |
| Storage Temperature | -40 °C to +85 °C |
| Relative Humidity | 5% to 95% non-condensing — rated for water treatment and food processing environments |
| Power Consumption | Supplied via PLC-5 chassis backplane |
| Weight | 900 g (as shipped) |
| Firmware | Factory-loaded; field-upgradeable via RSLogix 5 |
| Certifications | UL Listed, CE Marked, CSA Certified |
Why Engineers Specify This Model
1. In brownfield SCADA migration projects, the 1775-GA delivers zero-modification PLC-5 integration because it uses the original backplane pinout and firmware interface, meeting Rockwell Automation backward-compatibility specifications without chassis re-wiring.
2. In multi-drop SCADA polling applications across 64-node plant networks, the 1775-GA delivers deterministic token-passing latency because DH+ uses a controlled-token protocol rather than CSMA/CD, meeting ISA-99 network performance requirements for process control.
3. In long-distance field wiring across oil & gas plant sites, the 1775-GA delivers 3,048 m cable reach at 57.6 Kbps because the DH+ physical layer uses differential signaling on shielded twisted pair, meeting API RP 554 field wiring distance requirements.
4. In high-EMI environments such as automotive welding cells and VFD drive rooms, the 1775-GA delivers noise-immune communication because the DH+ differential signal rejects common-mode interference, meeting ANSI/RIA R15.06 electromagnetic compatibility requirements.
5. In MES and historian integration projects for food and beverage batch systems, the 1775-GA delivers reliable unsolicited messaging because DH+ supports both polled and peer-initiated data transfers, meeting ISA-95 Level 2–3 interface data availability requirements.
6. In water/wastewater SCADA networks with corrosive chemical atmospheres, the 1775-GA delivers sustained operation at up to 95% RH because the module’s conformal-coated PCB resists moisture ingress, meeting AWWA M2 environmental durability requirements.
Complete System Bill of Materials
| Component | Function | Relationship to 1775-GA |
|---|---|---|
| Allen-Bradley PLC-5 Processor (e.g., 1785-L40B) | Main CPU executing ladder logic and managing I/O | Host chassis into which the 1775-GA is installed |
| Allen-Bradley 1771 I/O Chassis | Backplane for PLC-5 modules and I/O cards | Physical housing and power supply for the 1775-GA |
| Belden 9463 Shielded Twisted Pair Cable | DH+ network trunk cable | Physical medium connecting the 1775-GA to the DH+ network |
| Allen-Bradley 1770-XY DH+ Connector Kit | Network termination and node tap connectors | Terminates the DH+ cable at the 1775-GA port |
| Rockwell RSLinx Classic / RSLinx Enterprise | PC-based DH+ driver and OPC server | Enables SCADA/MES software to communicate through the 1775-GA node |
| Rockwell RSLogix 5 Programming Software | PLC-5 ladder logic programming and firmware management | Used to configure node address and baud rate on the 1775-GA |
| Allen-Bradley 1785-ENET Ethernet Interface (optional) | Adds EtherNet/IP connectivity to the PLC-5 chassis | Complements the 1775-GA for dual-network brownfield architectures |
| UPS / Surge Suppressor (e.g., Phoenix Contact TRABTECH) | Power conditioning and transient protection | Protects the chassis and 1775-GA from voltage spikes on plant power |
Compliance & Industry Standards
UL 508 (Industrial Control Equipment) — Issued by Underwriters Laboratories. Confirms the module meets North American safety requirements for industrial control panels; required by most US and Canadian plant acceptance inspections and insurance underwriters.
CE Marking (EMC Directive 2014/30/EU + LVD 2014/35/EU) — Issued by Rockwell Automation’s Notified Body. Confirms electromagnetic compatibility and low-voltage safety for EU market installations; required for CE-marked control panels in European automotive and process plants.
CSA C22.2 No. 142 (Process Control Equipment) — Issued by CSA Group. Confirms compliance with Canadian electrical safety standards; required for installations under Canadian Electrical Code Part I in oil & gas and utilities facilities.
RoHS Directive 2011/65/EU — Confirms restriction of hazardous substances in electronic equipment; relevant for buyers in EU jurisdictions and for corporate ESG and sustainability compliance programs.
ISA-99 / IEC 62443 (Industrial Cybersecurity) — The DH+ protocol’s token-passing architecture provides inherent network segmentation, supporting Zone & Conduit models required by IEC 62443-3-3 for legacy OT network security in power generation and utilities.
Quality Assurance & Sourcing
Sourcing Channels: Konmask.com sources the 1775-GA exclusively from authorized Rockwell Automation distributors, certified surplus dealers with documented chain-of-custody, and decommissioned plant inventory with full traceability records. We do not source from unverified secondary markets.
4-Step Inspection Process:
Step 1 — Visual & Physical Inspection: Board-level examination for corrosion, component damage, remarking, or counterfeit indicators. Label authenticity verified against Rockwell Automation catalog records.
Step 2 — Functional Power-On Test: Module installed in a reference PLC-5 chassis and powered. DH+ node communication verified at both 57.6 Kbps and 115.2 Kbps baud rates using RSLinx Classic.
Step 3 — Firmware Version Verification: Firmware revision confirmed and logged. Modules with corrupted or non-standard firmware are rejected and not shipped.
Step 4 — Final Documentation & Packaging: Module serialized, test results logged, and packaged in anti-static ESD bag with foam insert. Lot traceability record attached to shipment.
Documents Available Upon Request: Test report, photos of physical condition, firmware version log, certificate of conformance, and sourcing declaration.
How to Source This Part
Step 1 — Submit Your Requirement: Contact Konmask.com via the inquiry form, email support@konmask.com, or call +0086 19859288691 with your part number (1775-GA), required quantity, and delivery timeline.
Step 2 — Receive Quote & Availability Confirmation: Our team responds within 24 hours with stock status, unit price, lead time, and available inspection documentation. Expedited sourcing available for urgent plant shutdowns and maintenance windows.
Step 3 — Order, Inspect & Ship: Upon order confirmation, the module undergoes final inspection and is shipped globally via DHL Express, FedEx International, or freight forwarder of your choice. Export documentation (commercial invoice, packing list, HS code 8537.10) provided for all international shipments.
Application-Specific FAQ
Q: Can the 1775-GA connect a PLC-5 to a modern FactoryTalk View SCADA system in a brownfield upgrade project without replacing the PLC?
A: Yes. In brownfield SCADA migration scenarios, the 1775-GA provides the DH+ node that RSLinx Classic bridges to the FactoryTalk View SE OPC server. The existing PLC-5 program and I/O wiring remain unchanged while the HMI layer is modernized — a common approach in automotive and food processing plants deferring full PLC replacement to a future capital cycle.
Q: How many PLC-5 racks with 1775-GA modules can coexist on a single DH+ segment in a large oil & gas or process plant?
A: DH+ supports up to 64 nodes per segment (addresses 0–63). Each 1775-GA occupies one node address. For networks exceeding 64 nodes — common in large refinery or utility SCADA systems — DH+ repeaters (e.g., Allen-Bradley 1770-KF2) bridge segments. Konmask can advise on network topology for your specific plant layout.
Q: Is the 1775-GA suitable for water treatment SCADA enclosures exposed to high humidity and chlorine or H₂S chemical vapors?
A: Yes. The 1775-GA is rated for 5–95% RH non-condensing, and Konmask verifies conformal coating integrity on all inspected units as part of the visual inspection step. For installations in particularly aggressive chemical environments (chlorine dosing rooms, H₂S exposure in wastewater headworks), we recommend specifying an additional enclosure purge or positive-pressure ventilation system for the PLC chassis.
© 2026 Konmask.com. All rights reserved.
Original Source: https://Konmask.com
Contact: support@konmask.com | +0086 19859288691