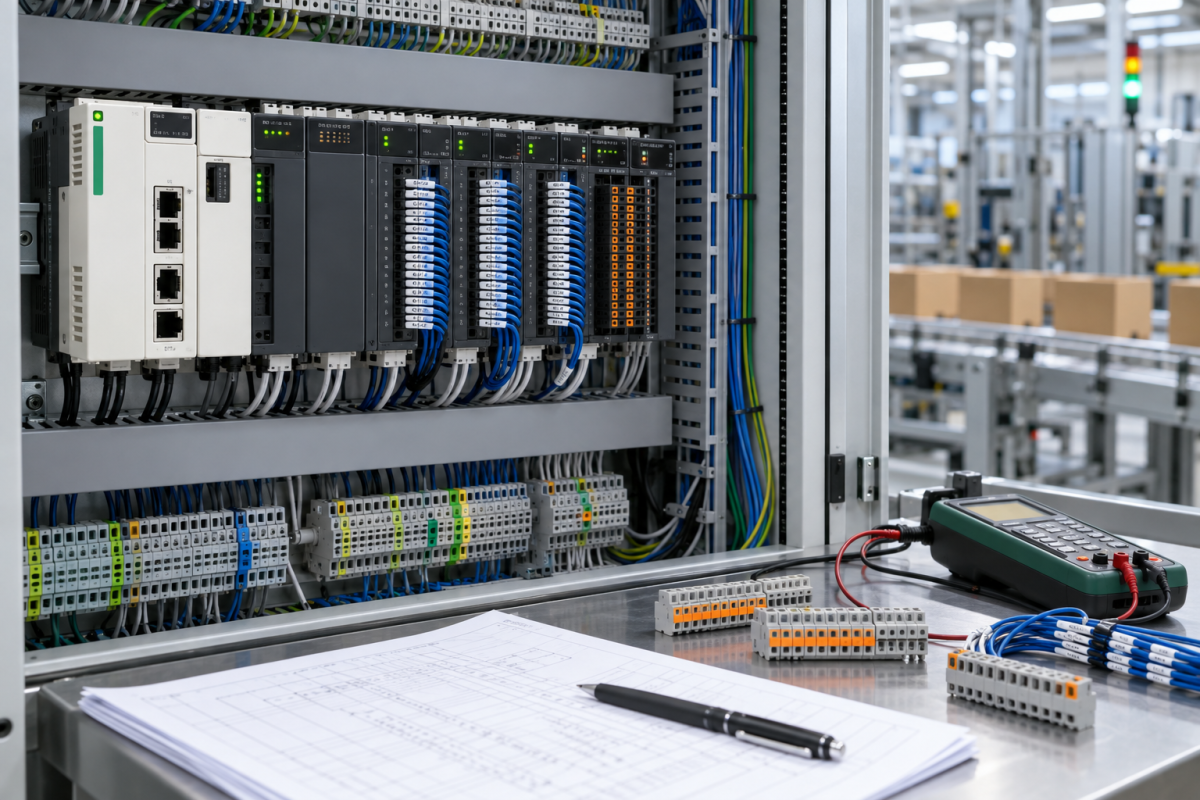
An M340 module swap looks simple when viewed from the aisle: release the terminal block, remove the module, install the spare, and restore power. The difficult part is proving that the 32 digital inputs or eight analog outputs still represent the same field reality after the work. A missing channel map turns a five-minute hardware action into a long commissioning exercise.
Schneider Electric updated its Modicon M340 controller setup guide in 2026, a useful reminder that current documentation and installed legacy details must be read together. The guide explains the platform; the plant record must explain how that particular rack is wired, configured, powered, and tested.
Build The Channel Map From Both Ends
For each occupied channel, record the PLC address, field tag, signal type, normal state or range, terminal number, common or reference connection, cable identifier, and the process consequence of a false value. Compare the cabinet drawing with the physical wire markers. Differences should be resolved before the terminal block is removed, not during restart.
Take one clear photograph of the complete module and terminal block, then closer views of the label, connector, keying, and wiring. Keep the image orientation consistent with the channel map so another engineer can follow it without guessing whether the drawing is viewed from the front or wiring side.
Digital Inputs Need More Than An LED Comparison
The BMXDDI3202K 32-channel digital input module concentrates many field states in one position. Confirm input voltage and sink/source arrangement, terminal-block type, commons, sensor power, debounce or filtering assumptions, and the configured module reference. A glowing input LED does not prove that the PLC variable, alarm, and interlock all interpret the point correctly.
Select representative channels from each common group. Test normal and abnormal states, check the PLC animation table, confirm HMI indication, and verify any permissive or trip logic affected. Where forcing is permitted, document who applies and removes it. Uncontrolled forces left after maintenance are a larger risk than a slow checkout.
Analog Outputs Must Be Checked As Loops
For the BMXAMO0802 eight-channel analog output module, capture the configured range, scaling, loop power arrangement, terminal block, cable shield, load resistance, fallback behavior, and the valve, drive, or actuator connected to every critical channel. Note whether the process device can be safely stroked or simulated during the outage.
Acceptance should compare the commanded PLC value, measured electrical signal, field-device response, and feedback returned to the control system. A correct 4-20 mA reading at the module is not enough if an isolator, marshalling terminal, positioner, or grounding problem prevents the process element from following the command.
Check Rack And Configuration Dependencies
Before ordering, confirm the backplane, rack slot, CPU firmware context, project software version, module configuration, terminal-block compatibility, and available cabinet depth. Inspect the rack connector for bent pins, contamination, or heat damage. If several modules report faults, investigate rack power and backplane health before replacing them one by one.
Archive the current project and export a readable channel list. Record the file location, date, responsible engineer, and method used to confirm that the backup matches the running controller. This prevents a hardware replacement from becoming an accidental configuration downgrade.
Write The RFQ Around The Installed Function
Specify full model, quantity, acceptable condition, terminal-block requirement, firmware or revision concerns, channel role, photos, delivery destination, and acceptance evidence. Ask whether the offered item includes the removable terminal block shown in the photo. That small scope question can decide whether the shutdown team can complete the replacement.
At receiving, compare the shipped label and connector face with the approved offer, inspect terminals and housing, record serial or revision details, and route the module to stores or bench test according to its intended use. Do not let an unverified spare become the only fallback for a critical rack.
Receiving Inspection Should Mirror The Channel Map
When the spare arrives, inspect it against the same evidence used to approve it. Confirm model and revision, housing and connector condition, terminal-block scope, keying, and channel count. Photograph the received item before it enters stores. If the module will remain on the shelf, attach the channel-map reference and the machine or rack for which it was qualified.
That discipline prevents a common surprise: a spare exists in inventory but lacks the terminal block, connector, or configuration evidence needed during an outage. Stores then becomes part of the recovery system instead of merely a location where electronics are kept.
FAQ
Can an M340 I/O module be ordered from the front label alone?
The full label is necessary, but terminal-block type, channel configuration, signal arrangement, rack context, and required accessories should also be confirmed.
Why test PLC logic when only an input module was replaced?
A valid electrical input must still reach the correct variable, HMI indication, alarm, permissive, or trip logic before the machine is considered recovered.
What is the minimum analog-output acceptance test?
Compare command, measured signal, field-device movement, feedback, alarms, and fallback behavior for representative critical loops.
Should the removable terminal block be included in the inquiry?
Yes. State whether it is required, provide photos, and verify connector and keying compatibility because offers may include only the electronic module.
Send Konmask the Modicon M340 module labels, rack and terminal photos, channel map, signal ranges, required accessories, condition preference, and outage date for a precise I/O spare inquiry.
© 2026 Konmask. All rights reserved. Official Website: https://konmask.com Inquiry: support@konmask.com | WhatsApp/Tel: +86 18359293191
