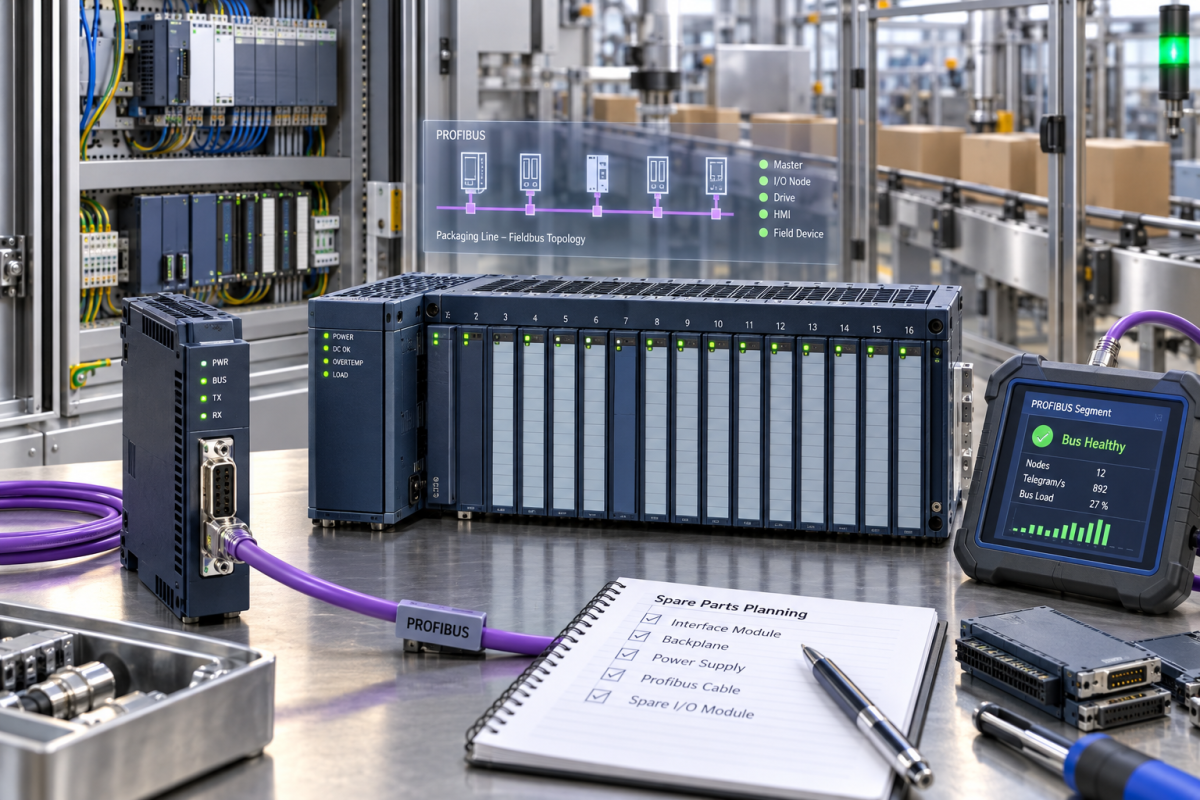
A Profibus segment fault can stop a machine even when the controller program is unchanged. For GE VersaMax and RX3i sites, bus recovery depends on interface evidence, backplane condition, rack power, connector photos, and the test used to prove I/O health.
Konmask has recently covered PanelView, ET 200, ABB robot, and RX3i redundancy angles. Today’s article keeps GE present but shifts the intent toward fieldbus and backplane evidence.
Separate Bus Evidence From Rack Evidence
Record station role, Profibus address, interface model, cable path, termination, rack slot, backplane condition, power, LEDs, diagnostics, and the affected machine function.
The first product reference checked before drafting was GE IC200GBI001 VersaMax Network Interface Module | GBI Profibus DP. It belongs in the discussion because the article is about the same installed risk, not because a link is needed at the end of the page.
The second published reference was GE IC695CHS016LT Universal Backplane | PACSystems RX3i 16-Slot Rack. Using two real, public product pages gives maintenance and procurement a practical vocabulary for labels, suffixes, connectors, and acceptance evidence.
Fieldbus Faults Need Physical Detail
The same symptom can come from the interface module, connector, termination, grounding, cable shield, rack power, or backplane seating.
Ask suppliers for actual photos, connector condition, tested status, rack or module accessory scope, and any revision notes before approving shipment.
A spare request should be written like a compact engineering handover. It needs the installed part identity, cabinet location, accessories, field wiring, software or parameter dependency, observed symptom, and the test that decides whether the part is acceptable. Without that evidence, the buyer is forced to compare catalog names instead of recovery risk.
Acceptance Should Prove The Bus Segment
After replacement, verify module recognition, bus diagnostics, node visibility, I/O response, HMI status, alarm clearance, and controlled machine restart.
If the bus remains unstable, review termination, cable shield, grounding, power, addressing, backplane seating, and field-device health before rejecting the spare.
The plant should also record what remains unknown. Firmware, backup files, licenses, calibration records, communication schedules, safety validation, and loop checks are site responsibilities. A supplier can confirm hardware identity and condition, but system readiness is proven only when the installed function passes the plant test.
Procurement Notes For Maintenance Teams
Ask for actual photos before approving shipment. Front labels, side labels, connector faces, terminal screws, rack position, LED state, daughter boards, batteries, cable tags, and accessory kits can reveal compatibility details that a one-line part number hides.
Separate emergency recovery from planned inventory. An emergency purchase may accept narrower evidence and faster freight, while a shelf spare should have cleaner documentation because it may be used by a different shift months later.
Condition terms should be specific. Factory sealed, new surplus, refurbished, repaired exchange, tested used, and untested used carry different risk. The RFQ should state which conditions are acceptable and what test evidence must accompany the offer.
Do not treat similar modules as automatic substitutes. Older PLC, DCS, SIS, HMI, drive, motion, robot, and condition-monitoring families often change by suffix, firmware, termination, memory, channel isolation, communication option, or cabinet depth.
Receiving inspection should repeat the sourcing evidence check. Compare the delivered item to the approved photos, confirm accessory scope, inspect connectors and terminals, record serial or revision details, and decide whether the part goes to stores, bench test, or immediate installation.
If a substitute is proposed, define the engineering review before purchasing releases the order. The reviewer should check fit, function, firmware or parameter impact, communication behavior, field wiring, safety consequence, and rollback plan.
For multisite groups, use a common RFQ format but allow local acceptance rules. A utility pump, turbine train, safety loop, valve skid, motion axis, robot cell, and operator panel do not carry the same consequence, even when the part numbers look routine.
A useful blog article for engineers should help the reader do the next practical step. That is why today’s topic is tied to real published product pages, current industry monitoring, and the evidence needed to move from research to a quote.
The best inquiry is short but complete: brand, full model, quantity, acceptable condition, installed role, photos, failure symptom, deadline, destination, and the acceptance test. That information reduces rework and makes supplier answers easier to compare.
Keep the final record with the spare. Product link, supplier evidence, photos, test notes, and acceptance status become valuable when the same platform fails again or when management asks why modernization should be funded.
The search angle also matters. Engineers may search by model number, but purchasing teams often search by family name, system name, or failure mode. A good article and a good RFQ should support both paths without stuffing keywords or forcing irrelevant products into the conversation.
When official support is limited, the quality of the installed evidence becomes even more important. Legacy hardware can often be kept reliable, but only when the site can prove what is installed, what is interchangeable, and what test will protect production after replacement.
FAQ
What must match on a GE Profibus or backplane spare?
Match the interface or rack identity, bus role, connector style, power requirements, diagnostics, and recovery test.
Why include cable and termination photos?
Profibus faults often come from connector, shield, or termination problems rather than the module alone.
What should procurement send?
Send labels, rack photos, connector photos, bus address, fault symptoms, condition requirement, quantity, and deadline.
What proves recovery?
Stable bus diagnostics, visible nodes, valid I/O response, clear alarms, and approved machine restart.
Send Konmask the GE module labels, rack and connector photos, Profibus symptoms, backplane evidence, and deadline. We can help prepare a PLC bus spare RFQ.
© 2026 Konmask. All rights reserved. Official Website: https://konmask.com Inquiry: support@konmask.com | WhatsApp/Tel: +86 18359293191
